Aegis provides affordable, low power Wi-Fi sensor network solutions that make a ubiquitous sensing world come alive and a full line of controlled temperature cabinets. Laboratory, Pharmacy and Chromatography refrigerators and freezers which are designed to meet the dimensional and temperature requirements of the scientific community.
Which Is the Best Sanitary Napkin Making Machine in China?
Choosing the best Sanitary Napkin Making Machine in China requires more than comparing advertised production speed. A reliable decision must connect product quality, factory conditions, operating costs, and after-sales support. The market is expanding as menstrual-health awareness grows worldwide. The WHO and UNICEF Joint Monitoring Programme reports that roughly 1.8 billion people menstruate every month. Yet many still lack suitable products, private facilities, or reliable information. This creates pressure for manufacturers to produce affordable, safe, and consistent sanitary napkins.
Professional market research also shows continued growth in feminine hygiene products, including disposable sanitary napkins. Reports from Grand View Research and Smithers highlight rising demand for thinner designs, improved absorbency, sustainable materials, and efficient manufacturing lines. These trends influence machine selection directly. Buyers should examine production speed, SAP distribution, servo control, raw-material compatibility, dust management, noise levels, and reject rates. A machine may claim 1,000 pieces per minute. That figure means little if the line wastes material during frequent changeovers.
Dr. Marni Sommer, a respected menstrual-health researcher, has stated, “Menstrual health is a public health issue.” Her point matters to equipment buyers. A fast machine cannot solve every access problem. It must support dependable products that factories can maintain and scale responsibly. The best Sanitary Napkin Making Machine may therefore be different for every manufacturer. A large export plant may prioritize automation and remote diagnostics. A regional factory may value simple controls, flexible formats, and available spare parts. The comparison is not perfect. Some suppliers also publish optimistic data. Real factory trials, inspection records, and customer feedback deserve greater weight than brochures.
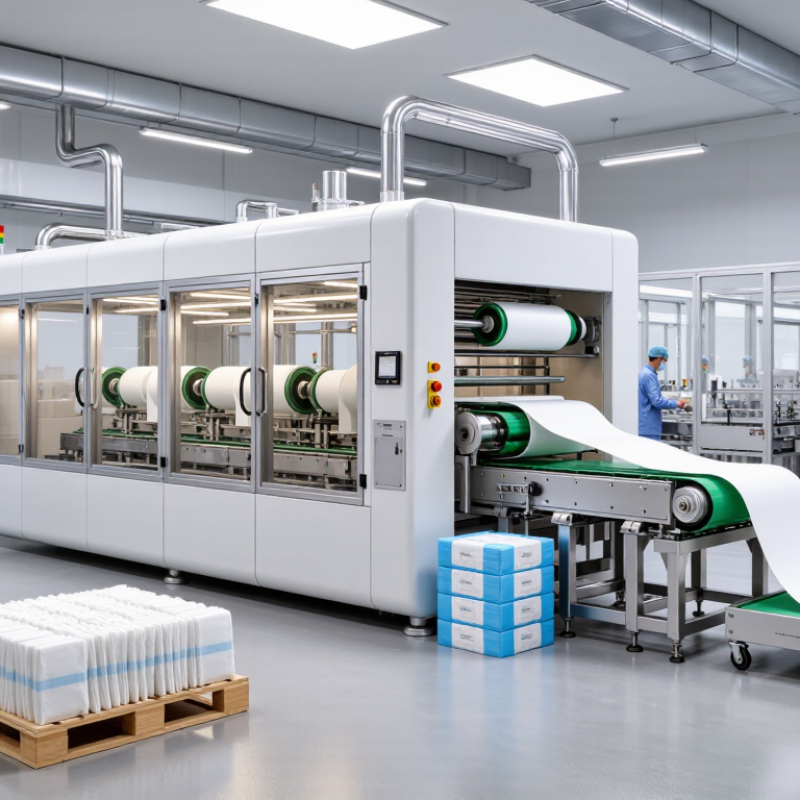
Table of Contents [Hide]
Understanding Sanitary Napkin Making Machines and Their Main Functions
Choosing the best sanitary napkin making machine in China requires more than comparing production speed. A complete line converts fluff pulp, superabsorbent polymer, nonwoven fabric, film, adhesive, and release paper into sealed products. Its main functions include raw material unwinding, pulp forming, SAP dosing, core compression, ultrasonic or adhesive bonding, cutting, folding, and packaging. Quality sensors can detect missing cores, poor seals, and incorrect positioning. Small details matter.
According to Grand View Research, the global feminine hygiene products market was valued at approximately USD 23.6 billion in 2023. Demand is influenced by product comfort, hygiene awareness, and access in developing markets. A machine should therefore support different sizes, absorbency levels, wing designs, and surface materials. Some industrial lines advertise outputs above 1,000 pieces per minute, but actual speed depends on product structure, operator skill, material stability, and inspection settings. Speed alone is a weak buying criterion.
From practical evaluation, I would examine tension control, servo accuracy, dust removal, changeover time, and spare-part availability. The line should keep the absorbent core centered, even when the pulp density changes slightly. That is difficult. The UNICEF and WHO menstrual health data also show that affordability and reliable access remain global concerns, so excessive automation may not suit every factory. A lower-speed line with stable quality, clear maintenance records, and responsive technical support can be the more responsible choice. Trial production is essential before purchase. Photographs cannot reveal every weakness.
Contact Us
Phone
Toll Free: 1-800-796-2344
OH: 513 204 5837
PA: 215-281-9180
support@site_367d8ed1-a876-442b-a1d7-b1fc1cf4ed19